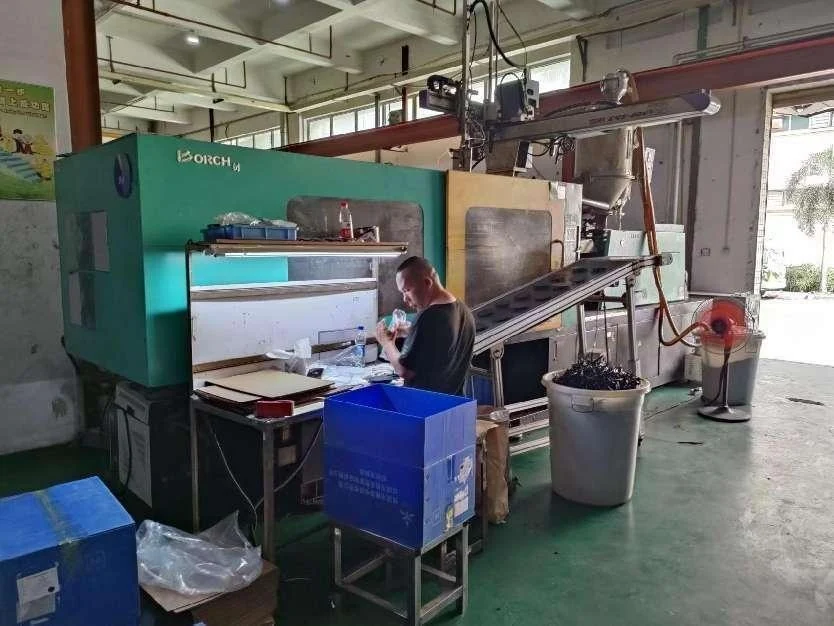
A mold that opens and ejects is not yet an accepted production process. Agree what each trial must demonstrate, what records are required and who approves the next step.
Name the trial stages before using T0 or T1
Different factories use T0, T1, T2 and final trial labels differently. In our project plan, each label should have a defined purpose, inputs and acceptance criteria. Likewise, 走模 may refer to dry mold cycling or a resin run in shop-floor conversation. Confirm the meaning rather than translating it into an assumed test.
| Activity | What our proposed plan records |
|---|---|
| Assembly and dry cycling | Tool identity, action sequence, travel, interferences, return, locks, sensors, lubrication and utility checks under the approved safe procedure. |
| Initial material trial | Machine, resin grade and preparation, runner setup, initial settings, filling observations, ejection and identified trial samples. |
| Correction and repeat trial | Issue list, approved design or process changes, revision traceability and evidence that each issue was resolved. |
| Dimensional and appearance approval | Samples by cavity, conditioning, measurement method, critical dimensions, cosmetic zones, finish and agreed function tests. |
| Production run-off | Agreed run duration, accepted cycle conditions, good output, rejects, stoppages, changeover and checks relevant to the actual production duty. |
| Customer-site acceptance | Receiving machine compatibility, installed utilities, setup, agreed repeat checks and open-item closure. |
A trial record should be reproducible
Keep the tool and product revisions, machine identification, resin lot, drying or conditioning records, mold and material temperatures, machine settings, cooling arrangement and sample timestamps. Identify cavities on the samples and report. A photograph of attractive samples without this context is not a process transfer package.
Measure the product under agreed conditions
Agree when and how the part is measured, the sample count, fixture and datum system, and treatment of flexible or moisture-sensitive materials. A statistical capability claim requires a suitable measurement system and an appropriate dataset from a controlled process; one good sample cannot establish production capability.
For two-shot and insert molding, include insert location, loading and detection, transfer alignment and the material interface. For silicone seals, include flash on functional surfaces and the specified sealing or assembly check. Automated lines need their own acceptance for handling, detection, reject separation and accepted output.
Separate tool acceptance from shipping approval
FAT and SAT can be used when defined in the contract; the abbreviations alone do not prescribe a universal test program. The customer should know which items are accepted, which remain open, and whether they affect shipment or production. Release packing only after the agreed records, samples, spares and outstanding-item responsibility are confirmed.
Trial and engineering support · Handover checklist · Plan a mold trial ↗
This is NewwaySmart’s proposed project checklist; each order defines its actual test scope. Dimensional acceptance reference: ISO 20457:2026. Follow the machine maker’s operating and safety instructions; this article is not an operating procedure.